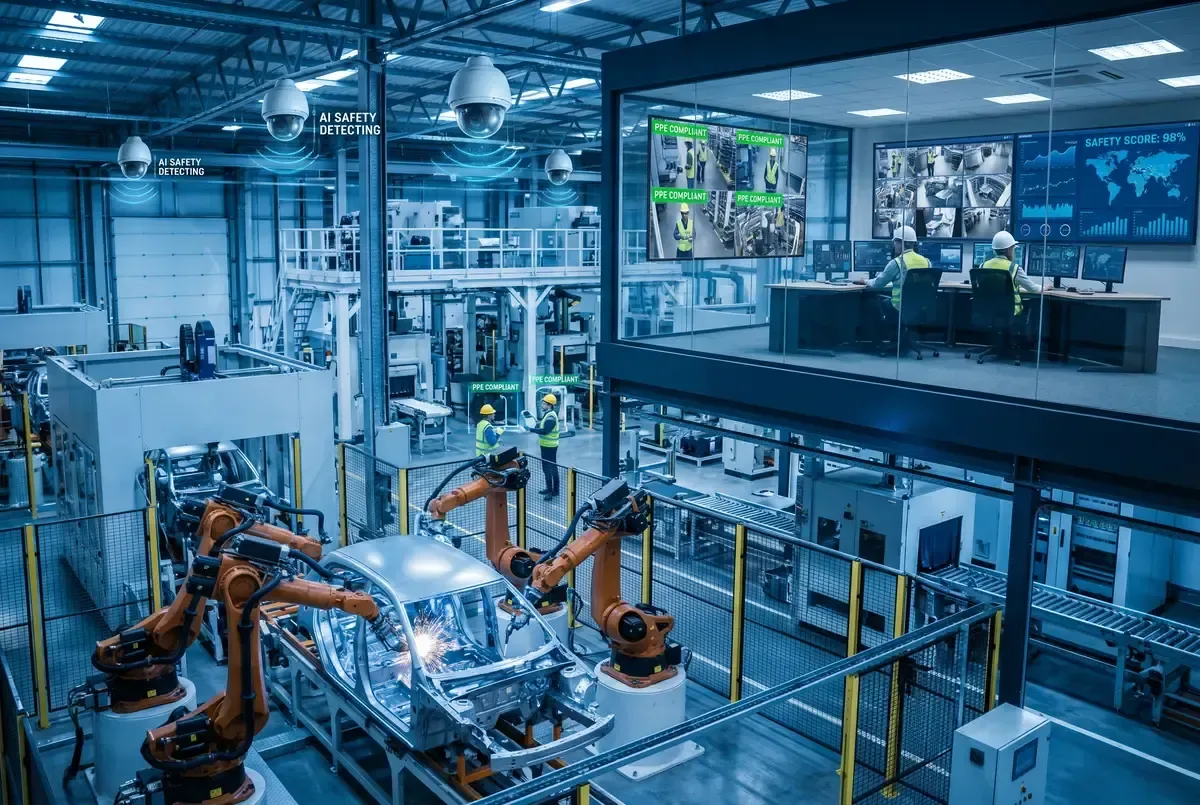
AI-powered PPE compliance, dangerous zone monitoring, equipment anomaly detection and fire/smoke early warning for industrial facilities. 24/7 intelligent protection.
Modern industrial facilities face complex safety challenges: workers entering hazardous zones without PPE, equipment running abnormally without early detection, and fire risks in high-temperature environments. Traditional manual inspection is insufficient.
AI-powered video surveillance transforms passive recording into active safety management — automatically detecting violations, triggering real-time alerts, and integrating with production systems to prevent accidents before they occur.
Workers without helmets, vests or safety shoes in hazardous zones
Early fire/smoke detection in high-temperature production areas
Unauthorized personnel entering dangerous machinery areas
Abnormal equipment behavior leading to production downtime
From procurement efficiency to business outcomes — measurable value at every level.
One-stop sourcing for complete system components. Verified compatibility reduces integration risk and procurement cycles.
Edge AI processing with <3s alert latency. ATEX-certified cameras for explosive environments. IP67/IP68 protection.
Automated violation detection replaces manual patrols. Predictive maintenance alerts reduce unplanned downtime by 40%.
60% reduction in workplace accidents. Full compliance with ISO 45001 and local safety regulations.
Comprehensive AI-powered safety monitoring covering all critical factory scenarios.
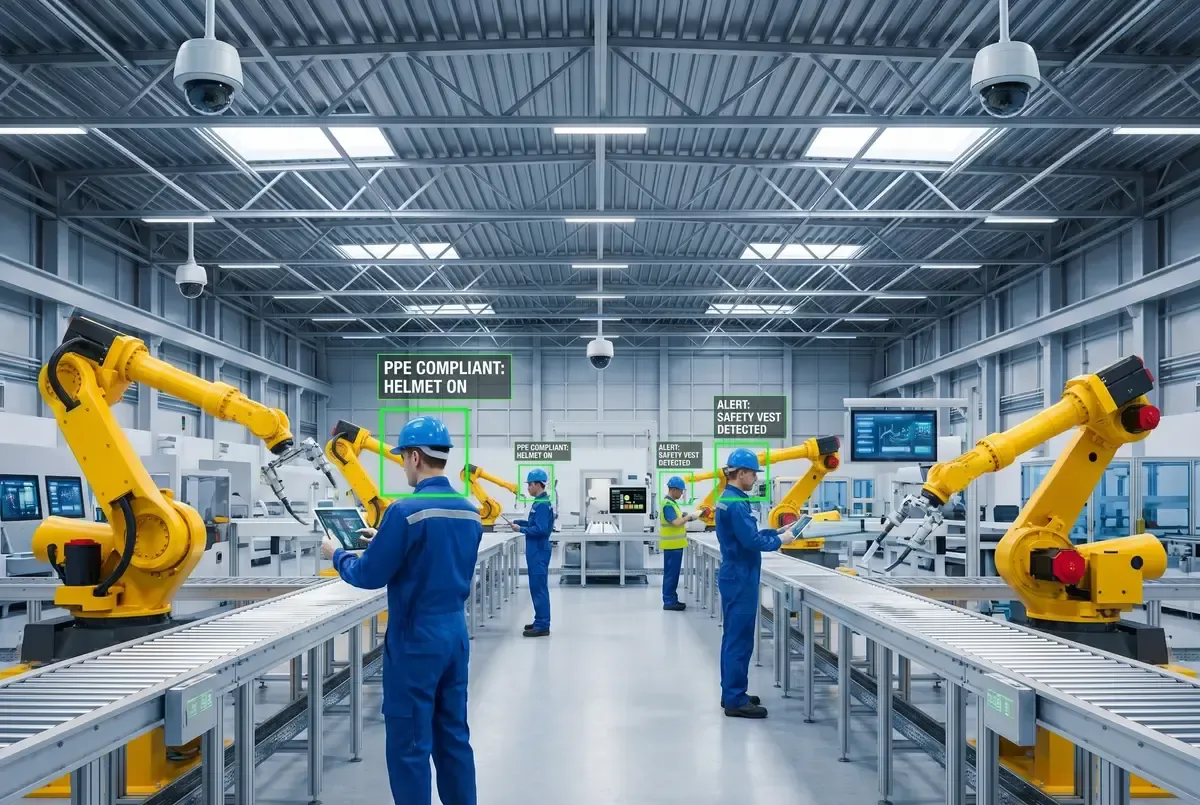
Real-time detection of safety helmets, vests, gloves, and safety shoes. Instant alerts for non-compliance with automatic evidence capture.
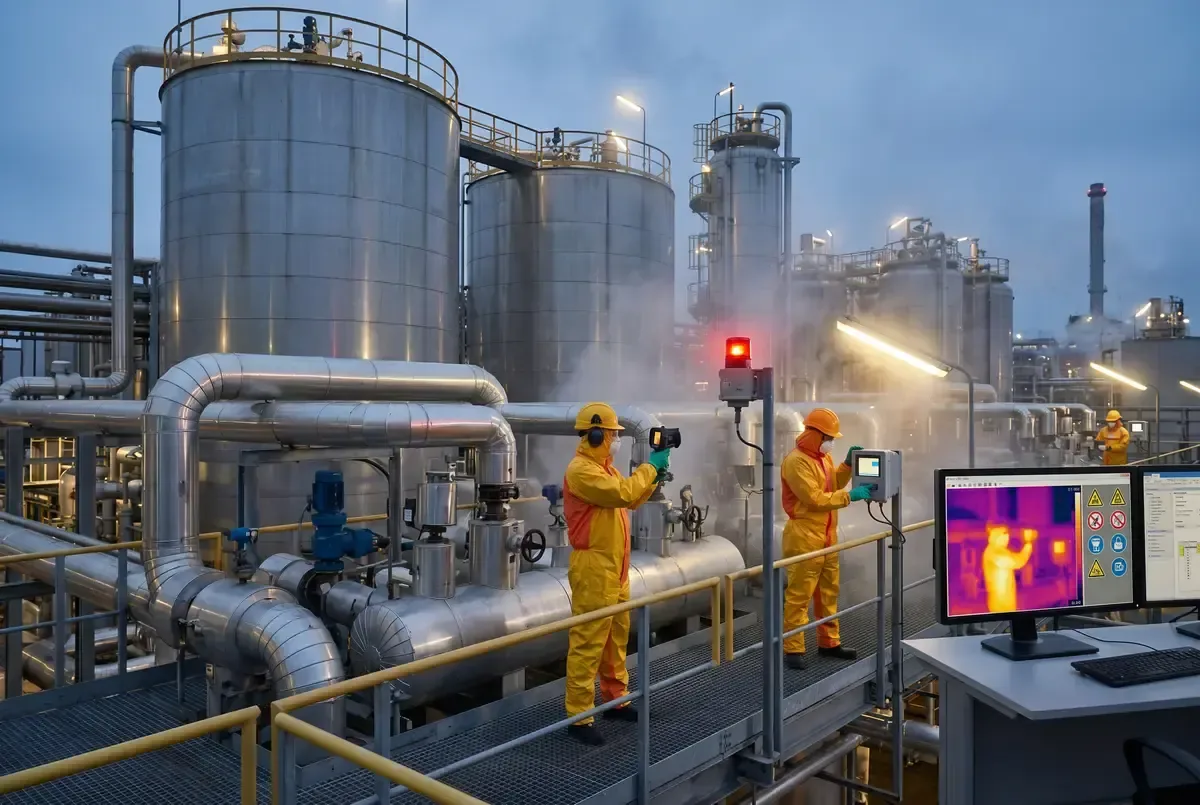
Thermal imaging detects overheating equipment. Vibration pattern analysis identifies abnormal machine behavior before failure.
Multi-spectral fire and smoke detection with <5s response time. Automatic linkage with fire suppression and evacuation systems.
Virtual perimeter fencing around machinery, high-voltage areas, and restricted zones. Immediate alert when unauthorized personnel enter.
Visual quality inspection integration, production flow monitoring, and worker behavior analysis to optimize efficiency.
Real-time monitoring via mobile app. Remote PTZ control, instant alert push notifications, and video playback.
Edge AI, PPE detection, 4-8MP, IP67, IR 30-50m
Fire/smoke detection, temperature measurement, ATEX optional
Industrial grade, -40°C~75°C, redundant power, managed
AI analytics, multi-channel recording, event management
Zone 1/2 certified, for chemical and gas environments
20-40x optical zoom, auto-tracking, perimeter patrol
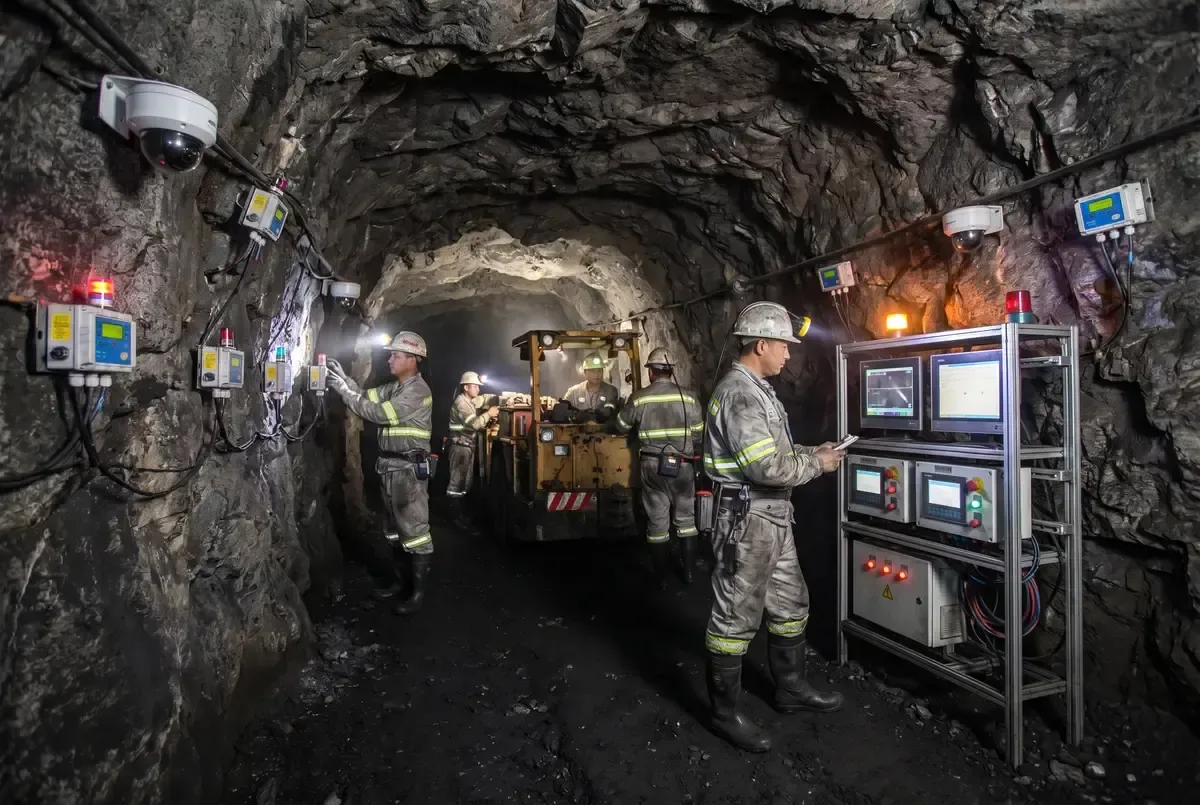
AI cameras capture real-time video streams across all production zones simultaneously.
On-device AI models analyze frames in real-time for PPE, behavior, and anomaly detection.
System identifies safety violations with bounding boxes, confidence scores, and timestamps.
Multi-channel alerts via screen popup, audio alarm, mobile push, and SMS within 3 seconds.
Automatic snapshot and video clip saved with metadata for compliance and investigation.
Automatic linkage with access control, PA system, fire suppression, and MES platform.
Safety officers receive mobile alerts and can remotely view live video and dispatch response.
Automated daily/weekly safety reports with violation statistics and trend analysis.
Assembly lines, stamping, welding, painting workshops — comprehensive PPE and behavior monitoring.
ATEX-certified cameras for explosive zones, gas leak detection, and hazmat handling compliance.
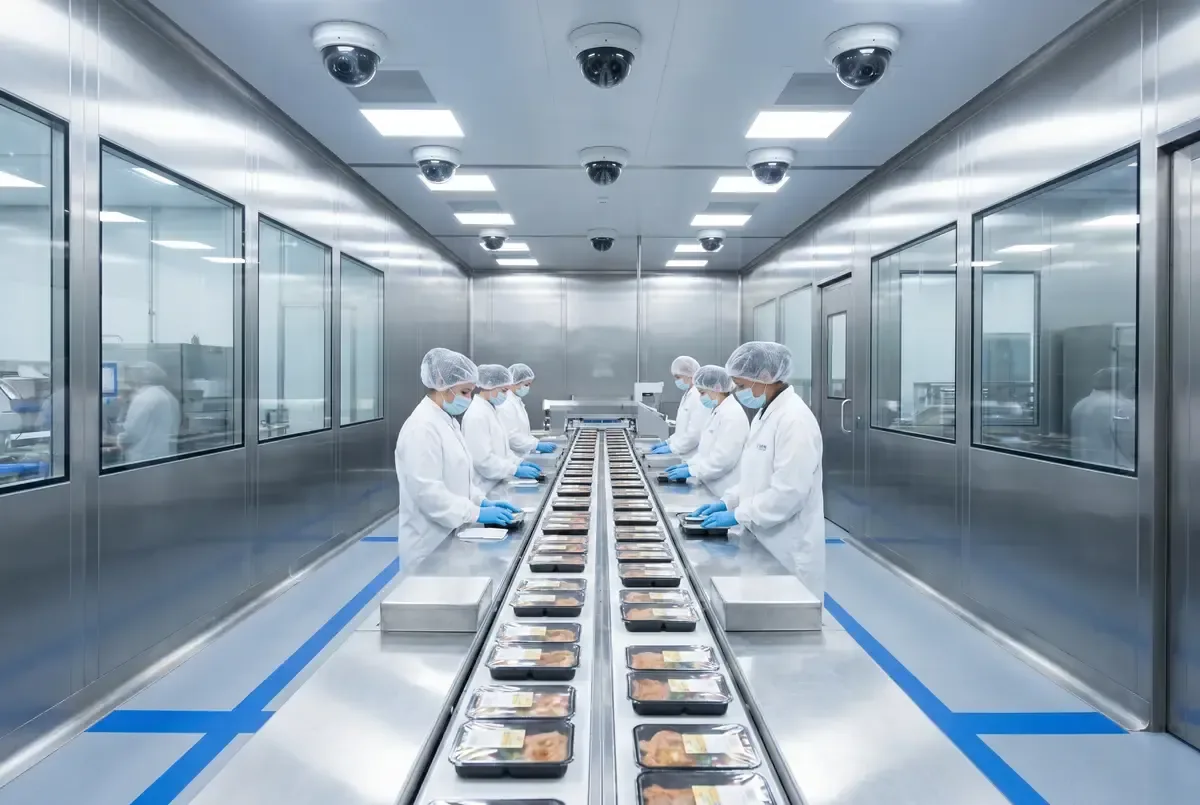
Hygiene compliance monitoring, clean room access control, and production traceability.
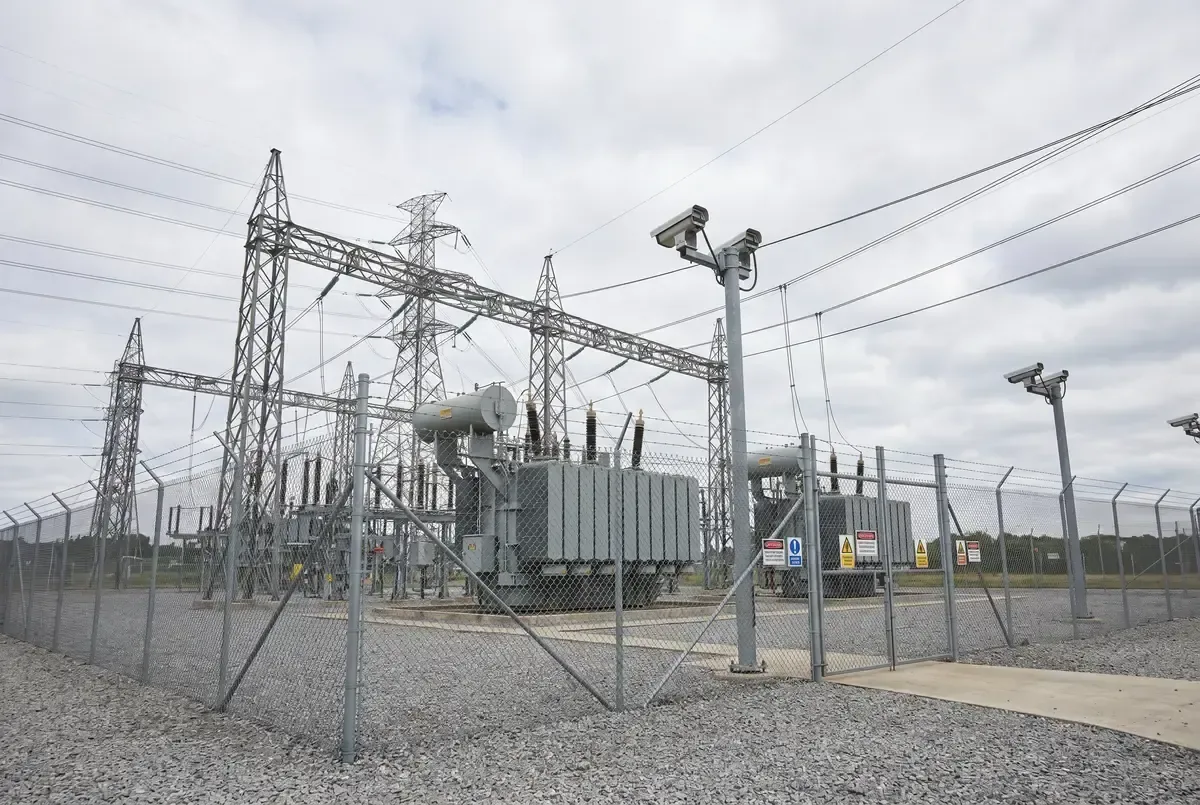
Substation perimeter security, equipment thermal monitoring, and unauthorized access prevention.
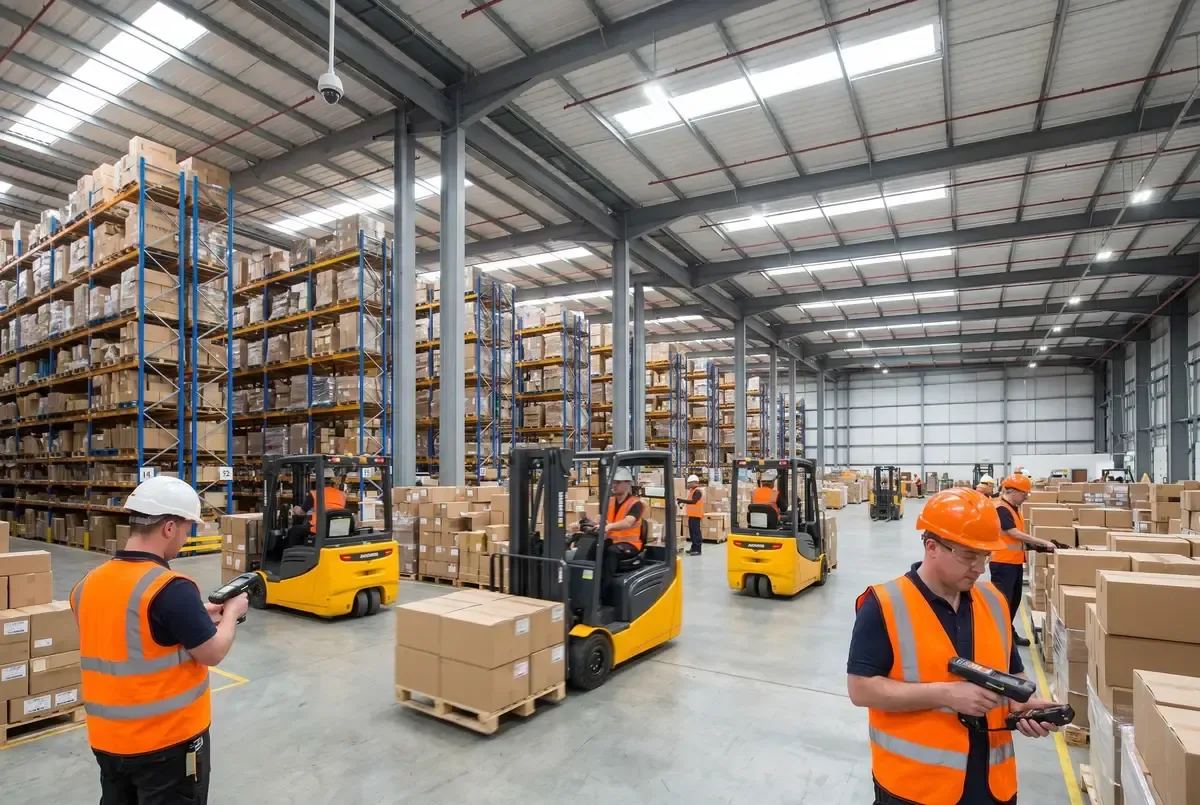
Forklift safety, loading dock monitoring, inventory management, and cold chain compliance.
High-temperature environments, crane safety, molten metal monitoring, and worker protection.
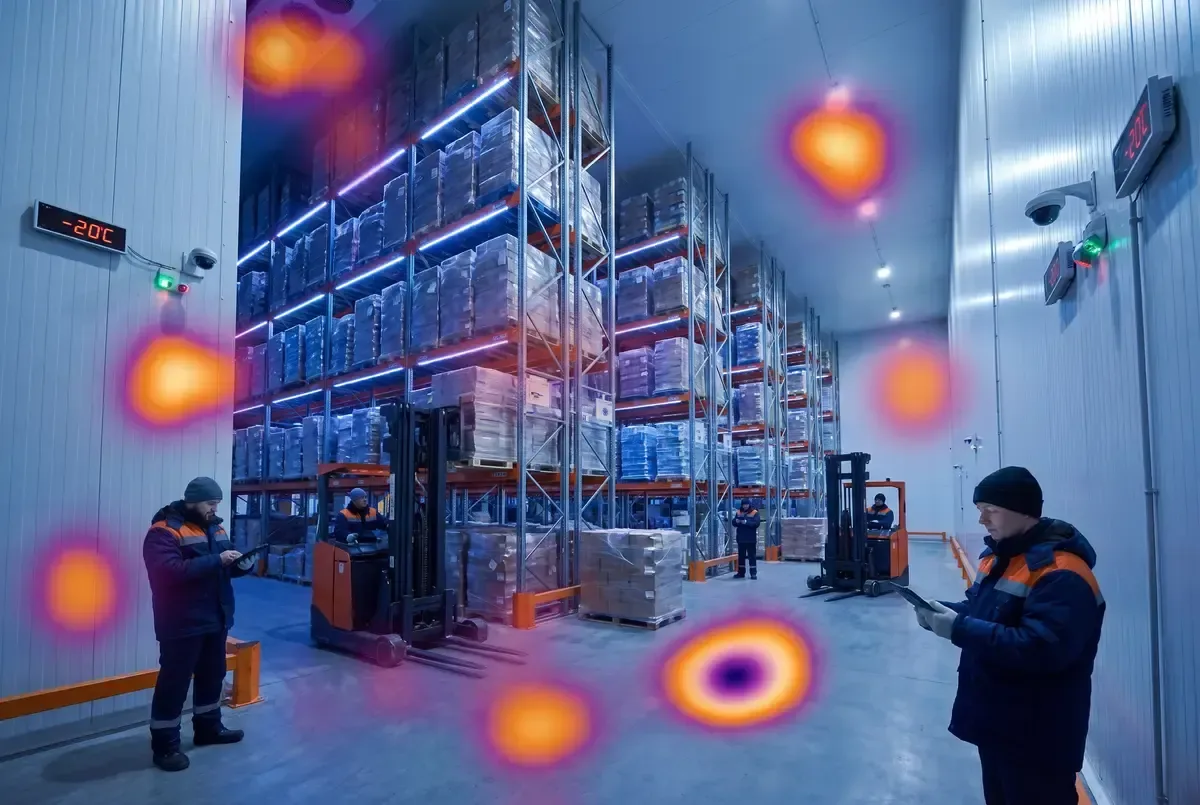
Temperature monitoring, cold storage compliance, product traceability.
View Solution →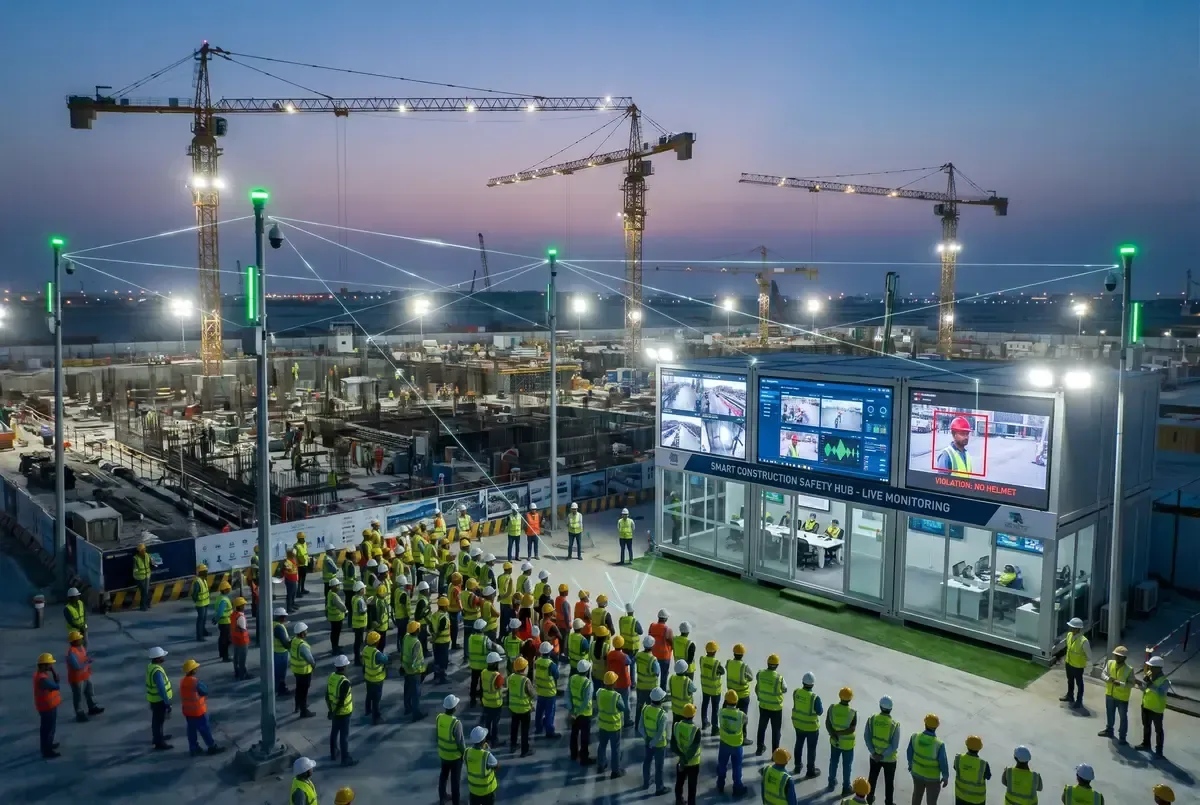
Crane safety, real-name attendance, dust monitoring, material anti-theft.
View Solution →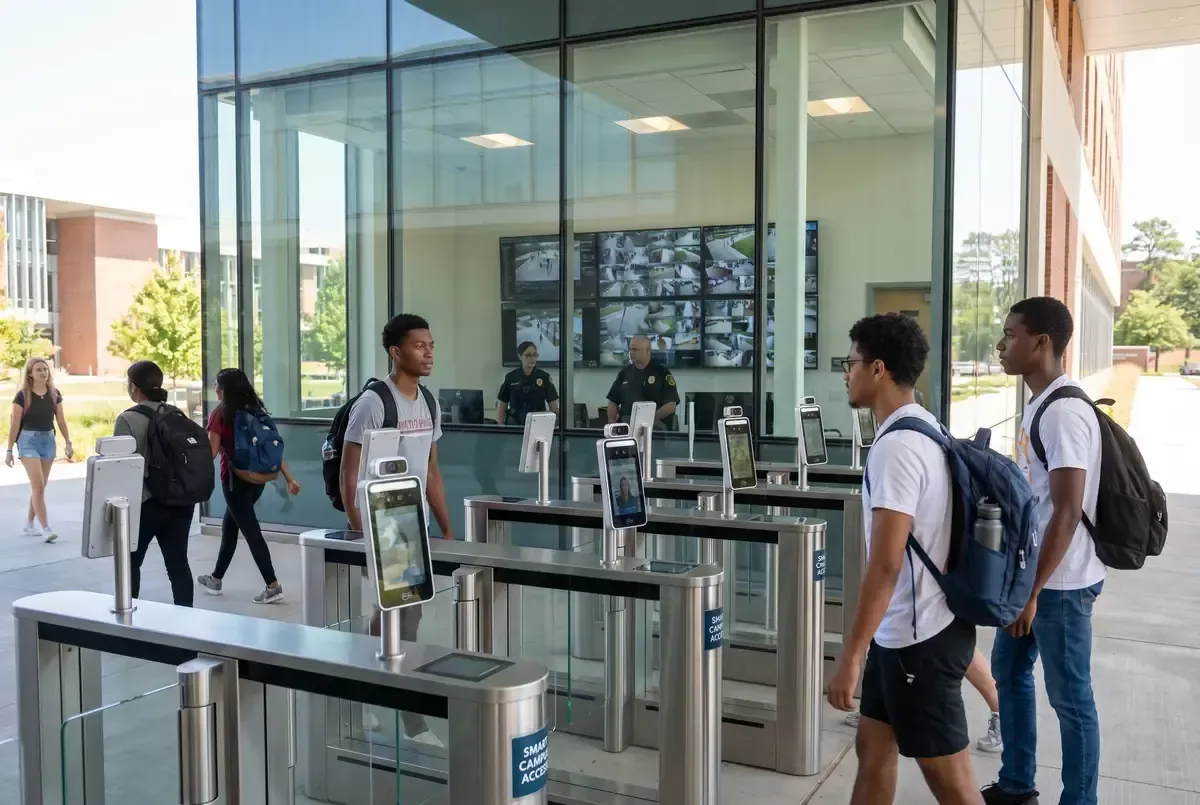
Behavior analysis, access control integration, visitor management.
View Solution →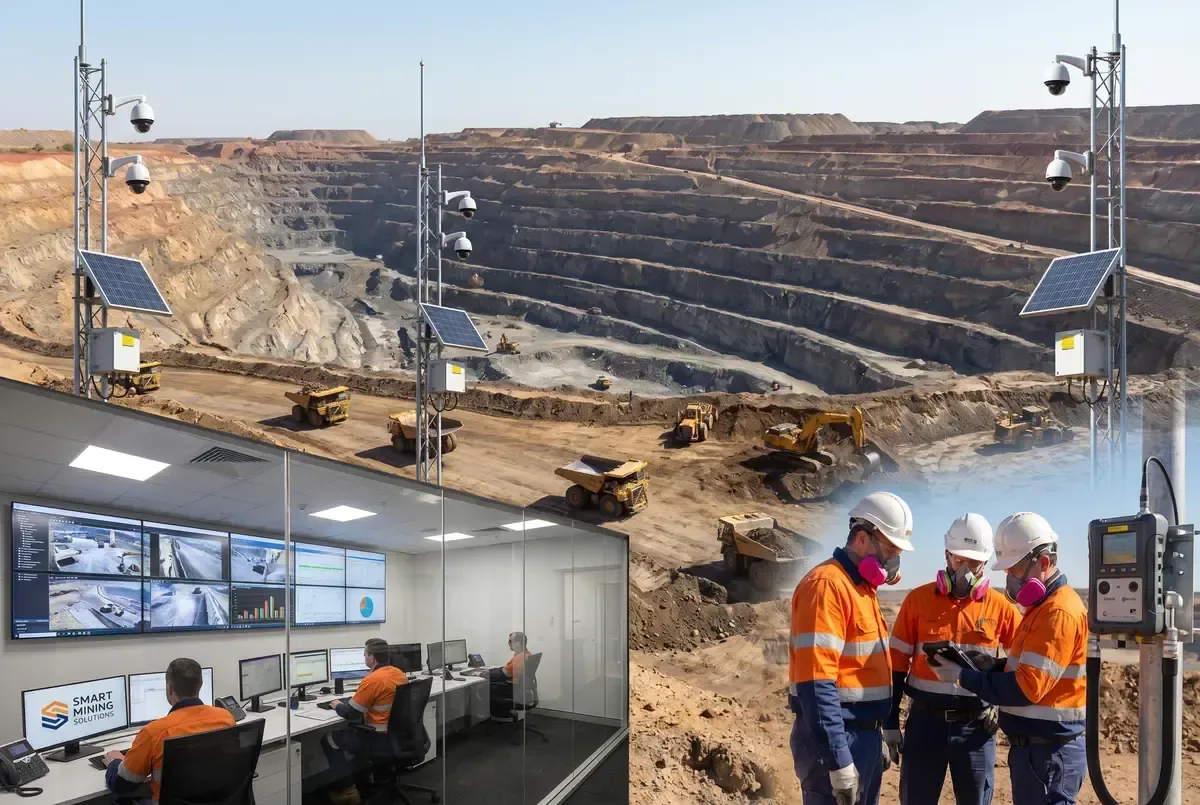
Underground tunnel monitoring, gas detection, personnel positioning.
View Solution →Tell us your factory scale, production type, and safety requirements. Our engineers will design the optimal surveillance system within 24 hours.